 English
 Deutsch

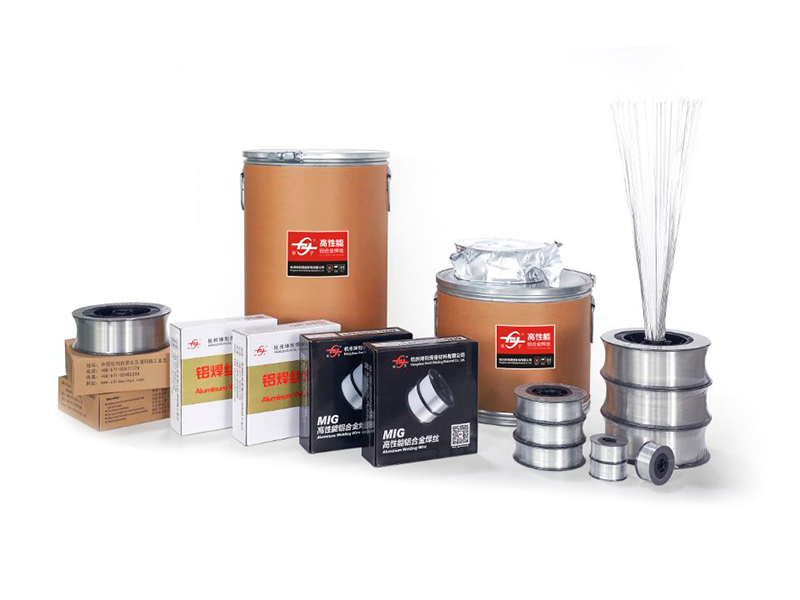
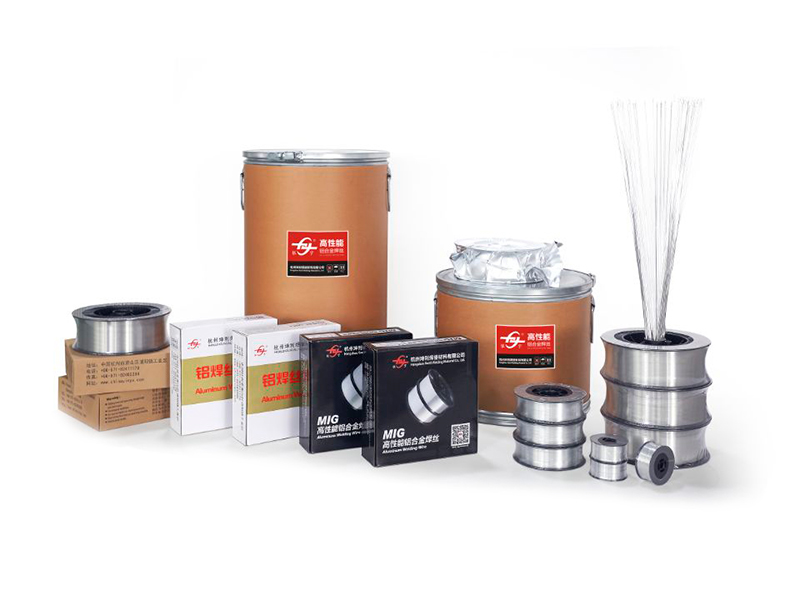
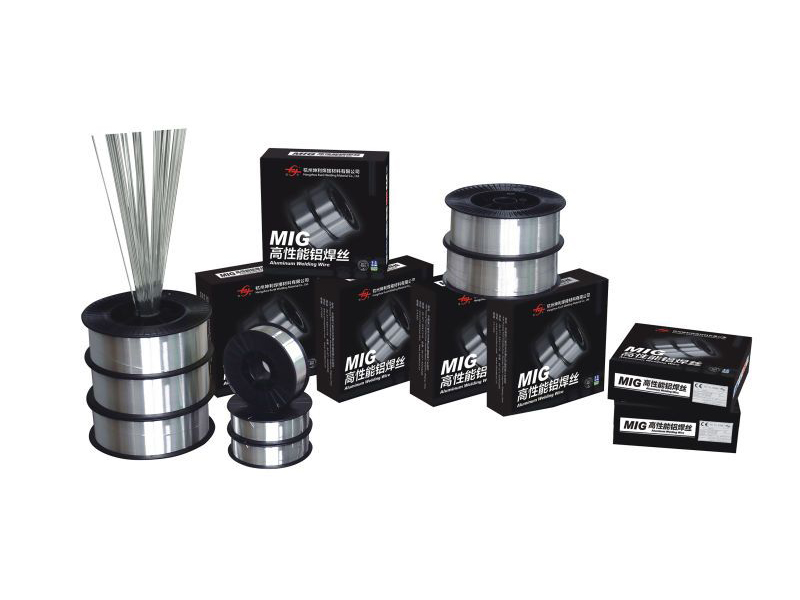
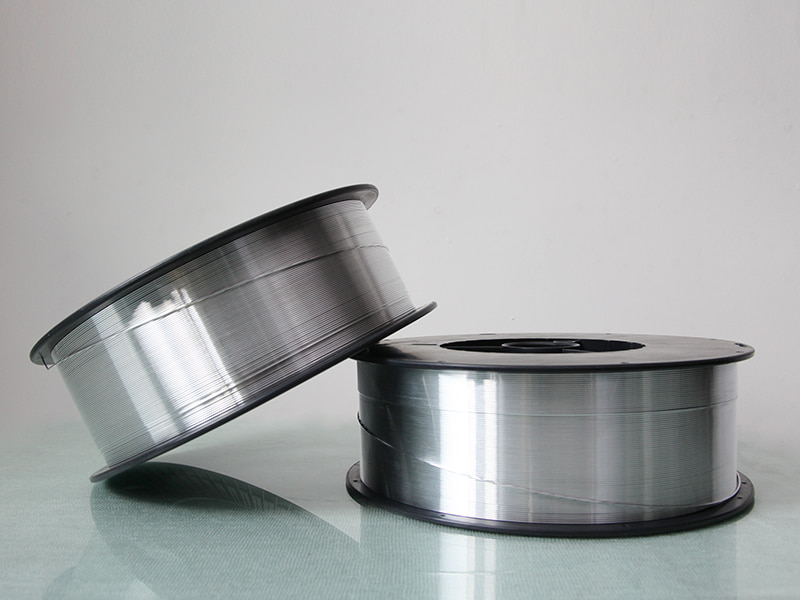
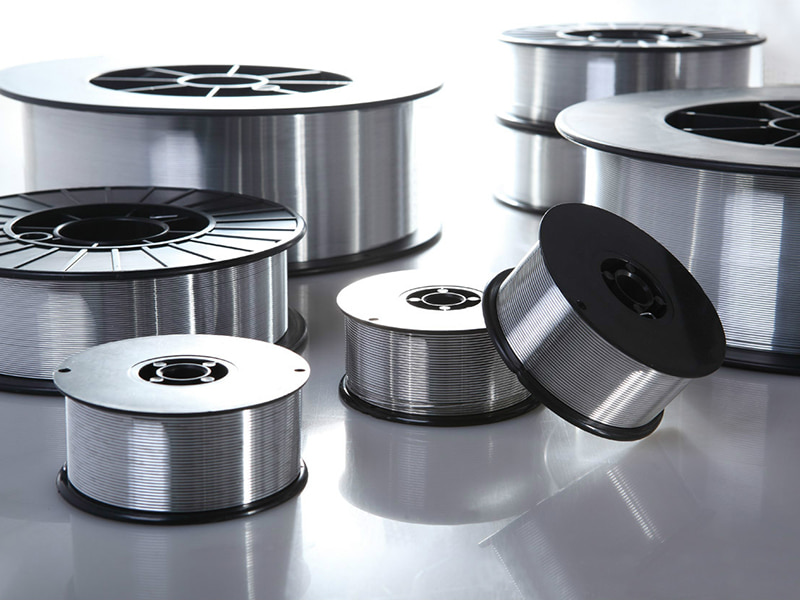
Aluminum Welding Wire
ER4047 Aluminum Mig Welding Wire
4047 is a 12% Silicon Aluminum filler metal which has excellent corrosion resistance and low melting point ensuring a very low number of deformations in the parent metal, recommended for welding alloys as 1060, 1350, 3003, 3004, 5052, 6060,6061,6063,etc. and casting Al alloys, such as 710.0,711.0.
E-mail: rich@chinayinyu.com
Contact Us
Al-Si12 Eutectic Alloy
ER4047 Aluminum Welding Wire
High Silicon Content | Brazing & Fusion Applications
11-13%
Silicon Range
577-582°C
Eutectic Melt
0.35-0.45 S/cm
Conductivity
ER4047 is a near-eutectic aluminum-silicon filler metal containing 11.0% to 13.0% silicon. This composition provides the lowest melting point among aluminum alloy welding wires, making it suitable for brazing applications and welding of thin-gauge materials. The high silicon concentration produces a fluid weld pool with reduced solidification shrinkage. Silicon also minimizes the formation of brittle intermetallic compounds when joining aluminum to coated steels or dissimilar metals.
Density (solid) 2.65 g/cm³
Electrical Resistivity 46 nΩ·m
Thermal Conductivity 155 W/m·K
Coefficient of Expansion 21.5 µm/m·K
Core Performance Attributes
Eutectic Fluidity
The 11-13% silicon composition produces a narrow freezing range of only 5°C, allowing the weld pool to flow readily into tight gaps and complex joint geometries. This characteristic supports brazing of lapped joints and repair of cast aluminum components.
Hot Crack Mitigation
High silicon content increases the volume fraction of eutectic phase at grain boundaries, accommodating thermal contraction strains during solidification. This reduces cracking susceptibility when welding high-magnesium 5xxx alloys or when dilution levels vary.
Brazing Compatibility
The low liquidus temperature (582°C) enables dip brazing and torch brazing of aluminum assemblies without melting the base material. Joint strength reaches 120-150 MPa in properly configured lap joints.
Porosity Control
Silicon acts as a deoxidizer, reducing hydrogen solubility in the molten weld pool. This results in lower porosity levels compared to pure aluminum fillers, particularly when welding anodized or oxidized surfaces.
TECHNICAL DATA SHEET
Wire Diameters
0.8mm · 1.0mm · 1.2mm · 1.6mm · 2.4mm
Precision ground, ±0.007mm tolerance
Surface Treatment
Shaved + Degreased + Oxide Controlled
Surface oxygen content below 80 ppm
Spooling Configuration
D200 / D300 / K300 / Pay-off drums
Layer wound with traverse pitch 0.85-1.1mm
Conformity Standards
AWS A5.10 (ER4047) · ISO 18273 (S Al 4047A)
CE certified for pressure equipment
⸬
Industrial Application Matrix
HVAC & Refrigeration
Brazed aluminum heat exchangers, condenser coils, evaporator cores, liquid line assemblies
Automotive Heat Transfer
Radiator tanks, heater cores, charge air coolers, oil coolers, battery cooling plates
Electrical Engineering
Bus bar joints, transformer windings, capacitor casings, aluminum to copper transitions
Additive Repair
Restoration of aluminum die castings, repair of porosity in cast components, build-up of worn surfaces
Lightweight Structures
Thin-wall tubing assemblies, honeycomb panel bonding, aerospace non-structural brackets
Power Generation
Generator housing repairs, cooling system components for transformers, bus duct fabrication
Process Optimization Guide
Incomplete fusion in brazed joints
Increase base metal preheat temperature to 250-300°C. Verify that filler metal is applied to the entire joint length. Maintain joint clearance between 0.05mm and 0.15mm for capillary flow action.
Base metal erosion or melting
Reduce torch dwell time and control heat input. For thin materials (below 1.5mm), use lower wire feed speed and travel speed above 40 cm/min. Consider pulsed GTAW parameters with peak current below 140A.
Grey or black residue on weld
Excessive silicon segregation or oxidation. Check shielding gas purity (argon 99.996% minimum). Increase gas flow to 18-22 L/min and verify absence of air drafts near welding zone.
Wire buckling at drive rolls
Switch to U-groove rolls with contact pressure set to lowest effective setting. Use extended Teflon liner with 0.1mm larger internal diameter than wire. Reduce tension on wire spool hub.
Reception & Storage Protocol
- Inspect packaging integrity upon receipt. Any damage to vacuum seal requires immediate wire inspection or rejection.
- Store spools in original packaging in areas free from airborne dust, oil mist, or chemical vapors.
- Maintain storage temperature between 10°C and 35°C. Relative humidity not to exceed 55%.
- Rotate stock using FIFO method. Maximum shelf life in unopened packaging is 36 months.
Pre-Use Conditioning
- Allow wire to acclimate to ambient welding temperature for 12 hours before opening the sealed package.
- For spools stored below 10°C, condition at 20-25°C for 24 hours to eliminate condensation risk.
- After opening, use wire within 72 hours. Partially used spools may be stored in dry cabinet at 30-40°C.
- Do not transfer wire between spools as layer winding pattern will be disrupted.
Welding Parameter Baseline
- GMAW (1.2mm): 18-22V, 100-160A, 100% Argon 18-22 L/min, stickout 15-20mm.
- GTAW (2.4mm): 80-140A, AC balance 65-75%, 100% Argon 10-15 L/min.
- Brazing (torch): Neutral flame, flux type FB3-S, base metal temperature 580-610°C.
ER4047 Aluminum Mig Welding Wire
Coming From China,
Marketing To The World.
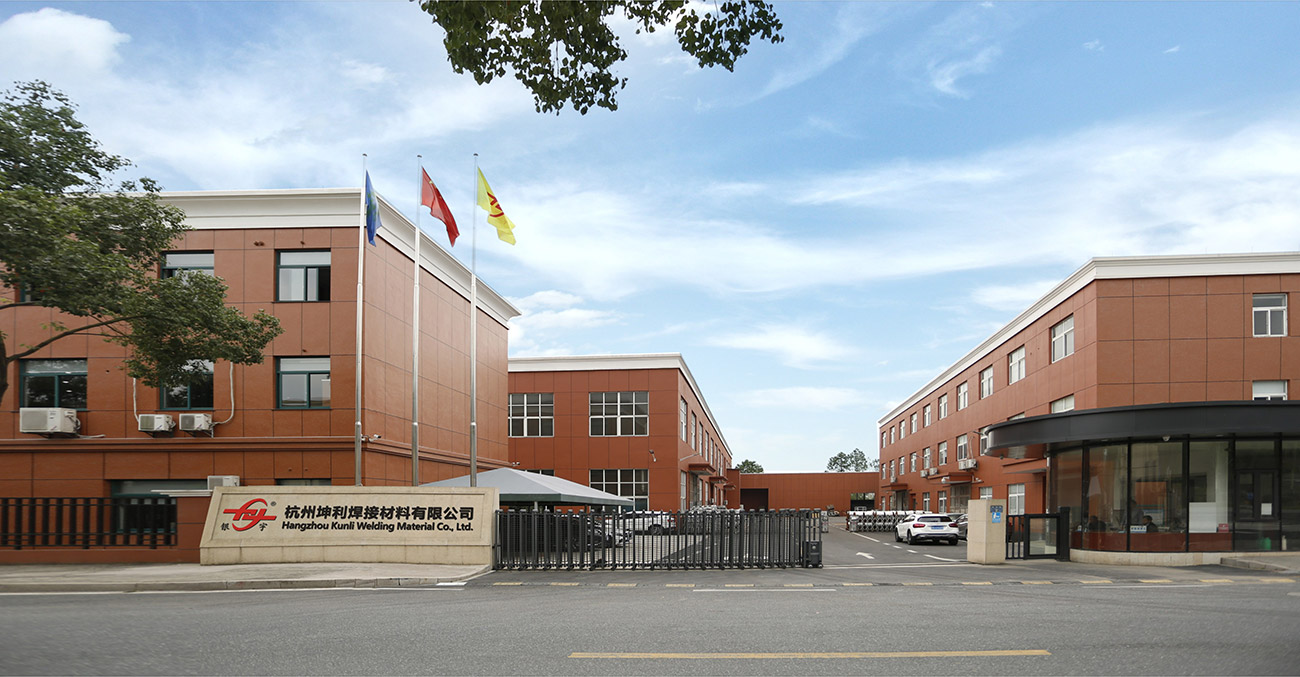
Hangzhou Kunli welding materials Co., Ltd. is located in the industrial zone of Puyang Town, Xiaoshan District, Hangzhou, Zhejiang Province. It is a high-technology and high-performance China Aluminum Welding Wire Manufacturers and
wholesale ER4047 Aluminum Mig Welding Wire factory. The company has more than 20 years of aluminum alloy wire production experience, with international advanced aluminum alloy welding wire manufacturing equipment, complete testing equipment, stable production process and strict quality control system. The high-performance
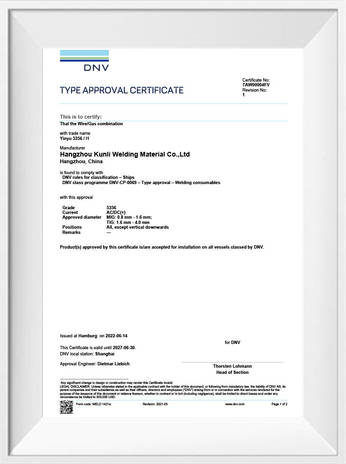
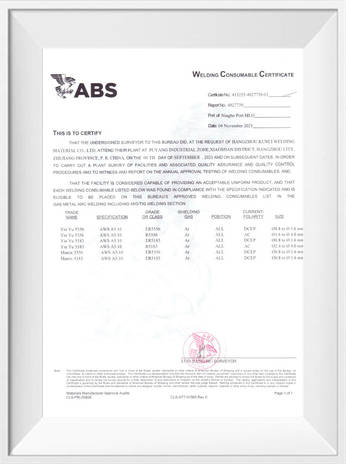
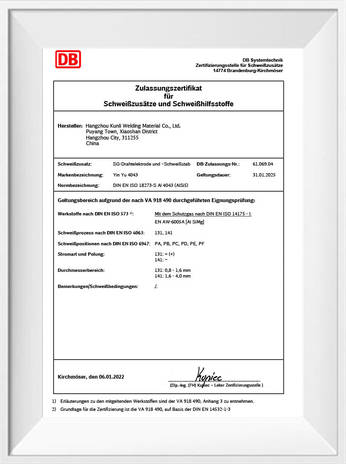
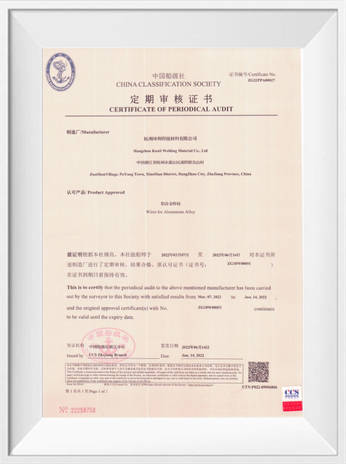
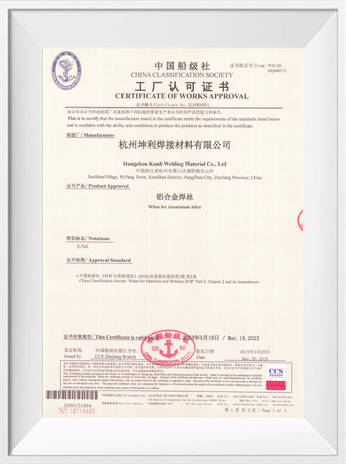
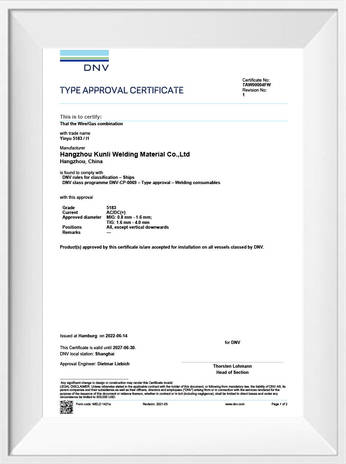
OEM/ODM ER4047 Aluminum Mig Welding Wire produced by the company has successfully passed a number of international authoritative certification, such as DB, CE, ABS, DNV, CCS, etc. We have more than 200MT production capacity per month and 50% was exported to over 30 countries such as USA, Mexico, Southeast Asia, Japan, Korea, Australia, New Zealand and etc.
-

30+
USED IN HEAVY INDUSTRY TECHNOLOGY SECTOR
-

35
YEARS OF RESEARCH AND DEVELOPMENT EXPERIENCE
-

200+
COOPERATIVE LARGE-SCALE R & D INSTITUTIONS
-

20+
GLOBAL TRADE COUNTRIES AND REGIONS
Coming From China,
Marketing To The World.
More than 90% of our field operators have professional and technical education background, and have many years of experience in equipment processing and assembly. It is precisely because of this united, dedicated, pioneering, skilled and experienced team that the company's technology and products can be continuously updated and improved.
GET IN TOUCH
Send Us a Message?
Related Products
-
 View More
5154 Aluminum Alloy Welding Wire
-
 View More
ER4043 Silicon Aluminum Welding Wire
-
 View More
ER4047 Aluminum Mig Welding Wire
-
 View More
ER5154 Al-Mg Alloy Wire
-
 View More
ER5087 Magnesium Aluminum Welding Wire
-
 View More
Aluminum Welding Wire ER5183
-
 View More
Aluminum Welding Wire ER5356
-
 View More
ER5554 Aluminum Welding Wire
-
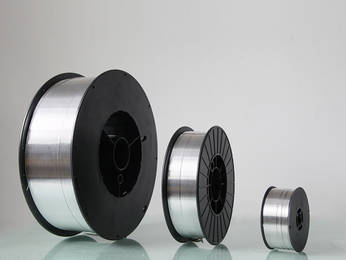 View More
ER5556 Aluminum Welding Wire
-
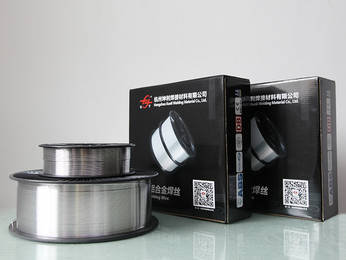 View More
ER1100 Aluminum Welding Wire
-
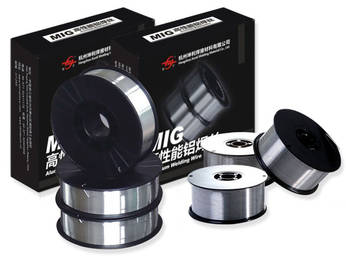 View More
ER5754 Aluminum Welding Wire
-
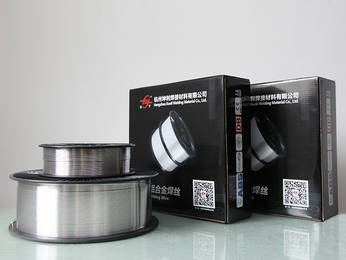 View More
ER2319 Aluminum Welding Wire
::: Last News :::
-
How Can Braided Aluminum Wire Support Flexible Connecti...
Sep 07, 2026
Electrical connections don't always sit in one fixed spot for the life of a machine. Many systems need conductors that ...
-
Custom Aluminum Welding Wire Solutions for Industrial A...
Sep 03, 2026
Consider a common scenario at a mid-sized fabrication plant: welding crews were reworking 6061-T6 frames for a transit ...
-
What Storage Practices Help Maintain Silicon Aluminum F...
Sep 02, 2026
Storage is easy to overlook when people discuss welding materials, mostly because attention naturally gravitates towar...
-
How Does Braided Aluminum Wire Construction Affect Flex...
Aug 31, 2026
Flexibility matters in a lot of ordinary wiring situations. A wire might need to wrap around a bracket, follow a machi...
Industry Information Extension
ER4047 Aluminum MIG Welding Wire
As a Er4047 Aluminum Mig Welding Wire.html manufacturer, we match product configuration to the application, operating limits, interfaces and acceptance criteria defined for each project.
As a specialized ER4047 Aluminum Mig Welding Wire manufacturer, Hangzhou Kunli Welding Materials Co., Ltd. produces a near-eutectic Al-Si12 filler metal with 11–13% silicon. This composition gives the lowest melting point among aluminum welding wires, making it the preferred choice for brazing, thin-gauge welding, and applications where fluidity and crack resistance are critical. Our wire is manufactured in our China factory with over 20 years of experience, using advanced equipment and strict quality control to ensure consistent performance.
Product Overview
ER4047 is a eutectic alloy with a narrow melting range of 577–582°C, providing excellent fluidity and reduced solidification shrinkage. It is designed for joining aluminum alloys such as 1060, 1350, 3003, 3004, 5052, 6060, 6061, and 6063, as well as cast alloys like 710.0 and 711.0. The high silicon content minimizes hot cracking and improves corrosion resistance, making it ideal for HVAC heat exchangers, automotive radiators, electrical bus bars, and repair of cast components.
Key Specifications
| Parameter | Value |
|---|---|
| Silicon Content | 11.0 – 13.0% |
| Melting Range | 577 – 582°C |
| Density | 2.65 g/cm³ |
| Electrical Conductivity | 0.35 – 0.45 S/cm |
| Thermal Conductivity | 155 W/m·K |
| Coefficient of Expansion | 21.5 µm/m·K |
Available Configurations
We supply ER4047 in a range of diameters and packaging to suit different welding processes and production scales:
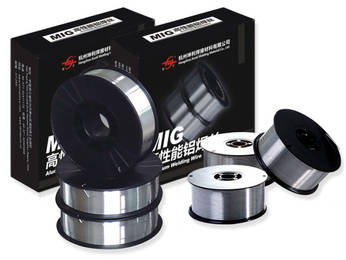
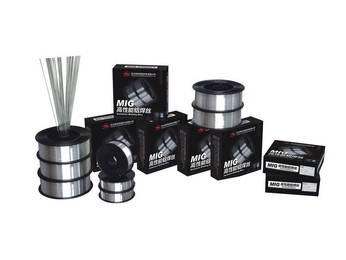
- MIG wire: 0.8, 0.9, 1.0, 1.2, 1.6, 2.4 mm – spools of 0.5, 2, 5, 6, 7, 9 kg
- TIG rods: 1.6, 2.0, 2.4, 3.0, 3.2, 4.0, 5.0 mm – 5 or 10 kg packs
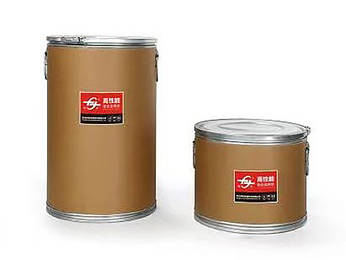
- Drum packaging: 40 or 80 kg for automated feeding
- Coils: 8–15 kg for manual or semi-automatic use
All wire is precision ground to ±0.007 mm tolerance, shaved, degreased, and oxide-controlled to keep surface oxygen below 80 ppm. Layer winding with traverse pitch 0.85–1.1 mm ensures smooth feeding and stable arc.
Application Fit
ER4047 is engineered for processes where low melting point and high fluidity are essential:
- HVAC & Refrigeration: Brazed aluminum heat exchangers, condenser coils, evaporator cores
- Automotive: Radiator tanks, heater cores, charge air coolers, battery cooling plates
- Electrical: Bus bar joints, transformer windings, aluminum-to-copper transitions
- Additive Repair: Restoration of die castings, porosity repair, build-up of worn surfaces
- Lightweight Structures: Thin-wall tubing, honeycomb panels, non-structural aerospace brackets
Welding Parameters
Optimal results depend on process and joint design. Our technical team can recommend specific parameters, but typical baselines are:
| Process | Parameters |
|---|---|
| GMAW (1.2 mm) | 18–22 V, 100–160 A, 100% Argon 18–22 L/min, stickout 15–20 mm |
| GTAW (2.4 mm) | 80–140 A, AC balance 65–75%, 100% Argon 10–15 L/min |
| Torch Brazing | Neutral flame, flux FB3-S, base metal 580–610°C |
Quality Assurance and Compliance
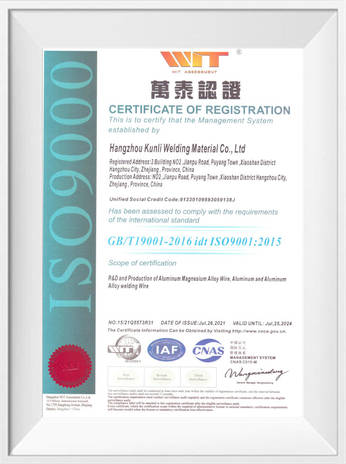
Our ER4047 is produced under ISO9001, ISO14000, and ISO18001 certified systems. Each batch undergoes chemical analysis, mechanical testing, and welding performance verification using advanced equipment like Shimadzu PDA spectrometers and OTC welding robots. The wire meets AWS A5.10 (ER4047) and ISO 18273 (S Al 4047A), and is CE certified for pressure equipment. We also hold DB, ABS, DNV, and CCS certifications, supporting marine and structural applications.
Storage and Handling
To preserve wire quality, store spools in original packaging in a clean, dry area (10–35°C, RH <55%). Allow sealed packages to acclimate for 12 hours before opening. After opening, use within 72 hours or store in a dry cabinet at 30–40°C. Maximum shelf life in unopened packaging is 36 months.
Information We Use to Configure Your Solution
To prepare a precise quotation and technical proposal, we need the following project details:
- Base material alloy and thickness
- Welding process (MIG, TIG, brazing) and joint design
- Required wire diameter and packaging type
- Production volume and delivery schedule
- Any specific standards or certifications required
Our engineers use this information to recommend the optimal wire configuration and provide welding parameter guidance.
Related Products
Explore our full range of aluminum welding wires, including ER4043 Silicon Aluminum Welding Wire for general-purpose welding, ER5356 Aluminum Welding Wire for high-strength applications, and ER5183 Aluminum Welding Wire for marine-grade joints. For more options, visit our Aluminum Welding Wire category.
FAQs
What is the main advantage of ER4047 over ER4043?
ER4047 has a higher silicon content (12% vs 5%), giving it a lower melting point and superior fluidity. This makes it ideal for brazing and thin-gauge welding where tight gaps and minimal distortion are required.
Can ER4047 be used for welding 6061 aluminum?
Yes, ER4047 is recommended for 6061 and other 6xxx alloys. It provides good crack resistance and corrosion performance, though for higher strength requirements, ER5356 may be preferred.
What packaging options are available for automated welding lines?
We offer drums of 40 or 80 kg for continuous feeding, as well as spools with precise layer winding to ensure smooth wire payoff. Custom packaging can be arranged for specific line requirements.
How do you ensure consistent quality across batches?
Our production process includes strict incoming material inspection, in-process monitoring, and final testing of chemical composition, mechanical properties, and welding performance. Each batch is traceable and documented.
Do you provide technical support for welding parameter optimization?
Yes, our welding engineers can assist with parameter selection, troubleshooting, and even on-site support if needed. We work closely with customers to ensure successful implementation.
QUICK LINKS
PRODUCT
CONTACT US
-
Jianpu Road no.2 Puyang Town Xiaoshan District Hangzhou Zhejiang China 311255
-
+86-0571-82403878
-
+86-0571-82403208
-
rich@chinayinyu.com
MOBILE TERMINAL
BE THE FIRST TO KNOW
Copyright © Hangzhou Kunli Welding Materials Co., Ltd. Rights Reserved.
