 English
 Deutsch

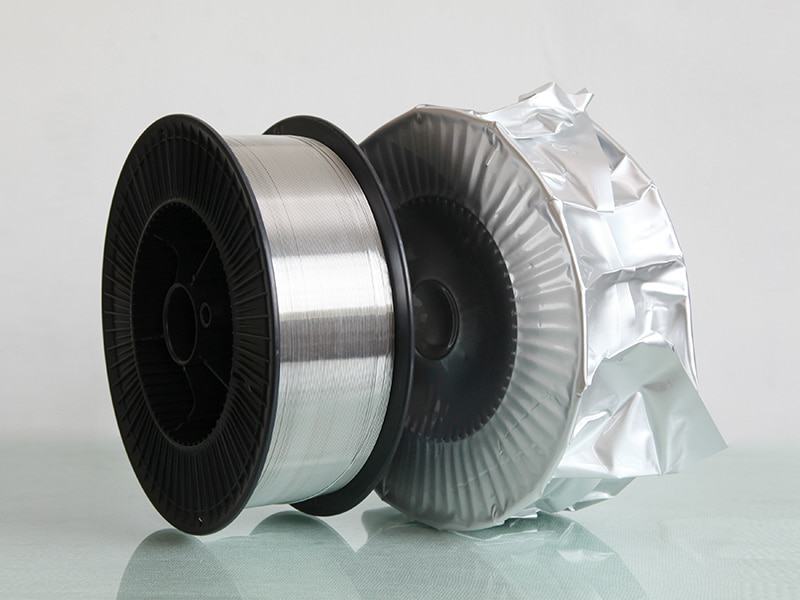
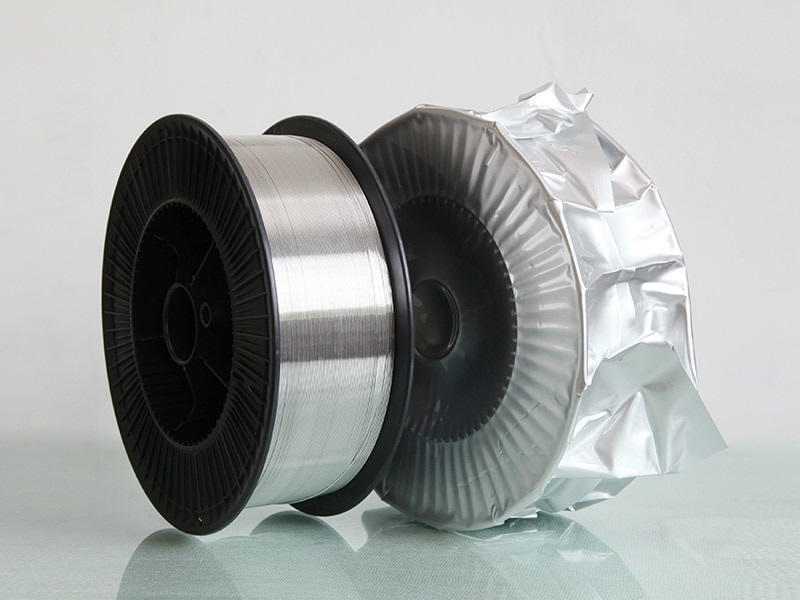
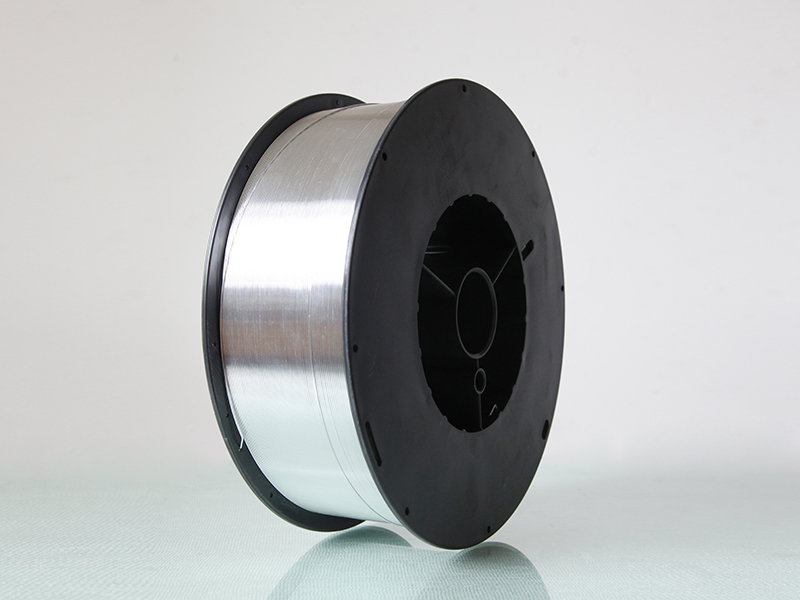
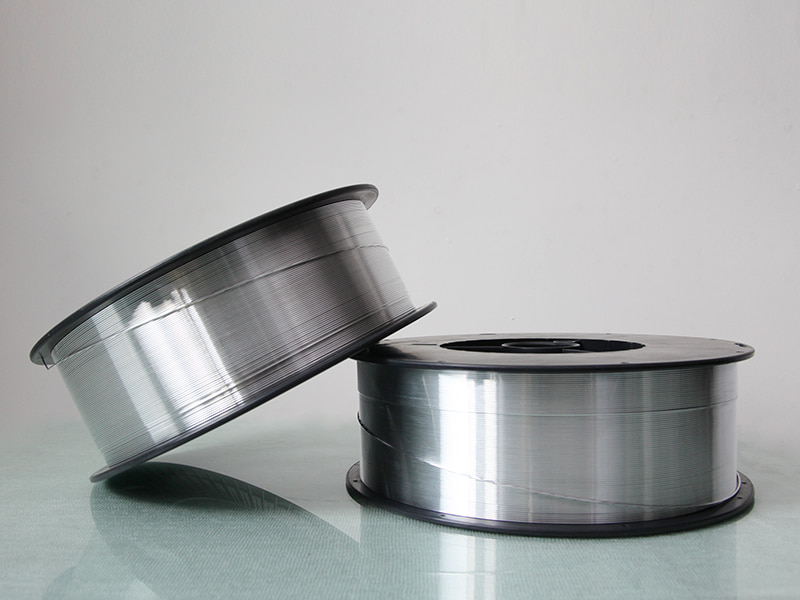
Aluminum Welding Wire
ER5154 Al-Mg Alloy Wire
Grade 5154, Al-Mg alloy wire is used for braiding in coaxial cable for shielding, with it's good performance.
Main Application: flexible coaxial cable, a variety of audio and video cable, vehicle signal cable, network cable, data transmission cable and so on.
E-mail: rich@chinayinyu.com
Contact Us
Al-Mg4.5Mn
ER5154 Aluminum Welding Wire
Magnesium-Manganese System | Marine & Structural Grade
3.1-3.9%
Magnesium
0.15-0.5%
Manganese
275-320 MPa
Tensile Range
ER5154 is a magnesium-manganese alloyed filler metal containing 3.1% to 3.9% magnesium with controlled manganese addition of 0.15% to 0.5%. This composition provides higher as-welded strength compared to ER4043 or ER5356 alternatives when joining 5xxx series base materials. The manganese content refines grain structure in the weld deposit, improving ductility and fatigue resistance. ER5154 maintains mechanical properties in service temperatures from -196°C to 65°C, supporting cryogenic and marine applications. The alloy system exhibits natural aging stability without heat treatment requirements.
Solidus: 570°C
Liquidus: 640°C
Elongation: 16-20%
Hardness: 75-85 HB
Technical Performance Framework
M
Strength Retention After Welding
The magnesium-manganese combination maintains 90-95% of base metal tensile strength in as-welded condition. No post-weld artificial aging required for structural applications.
C
Corrosion Resistance Profile
Passive oxide layer stability in salt spray testing exceeds 2000 hours per ASTM B117. Resistance to intergranular attack in chloride environments comparable to 5154 base alloy.
T
Thermal Stability
Mechanical property retention at elevated temperatures (150°C for 1000 hours) shows less than 8% reduction in ultimate tensile strength.
W
Weld Metal Soundness
Controlled hydrogen content below 0.12ml per 100g aluminum produces radiographic Class I quality welds without centerline porosity or micro-fissuring.
specification data
Diameter Offering
0.8mm | 1.0mm | 1.2mm | 1.6mm | 2.0mm
+0 / -0.008mm tolerance
Surface Condition
Precision shaved + ultrasonic degreased
Residual lubricant: Below 0.003g/kg
Packaging System
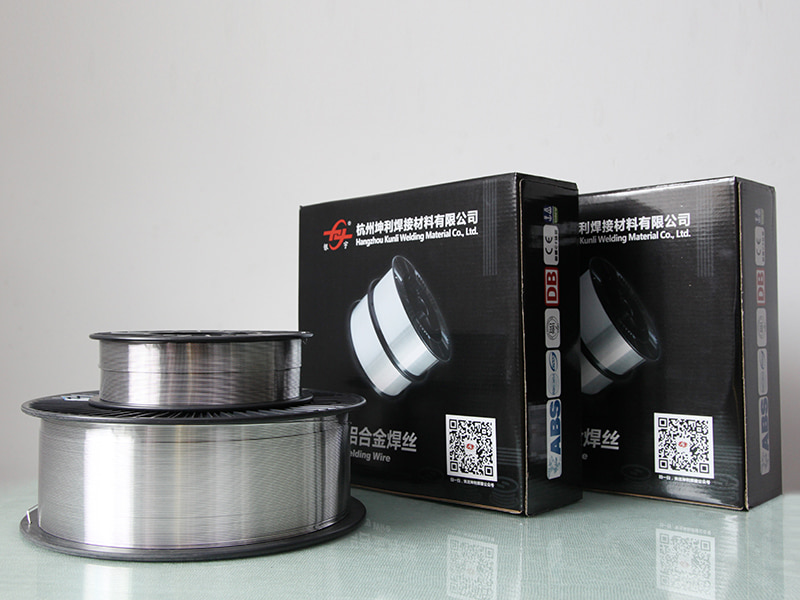
D300 plastic spool (7kg) · K355 drum (50kg) · Pay-off bin (200kg)
Layer wound with reverse bend control
Certification
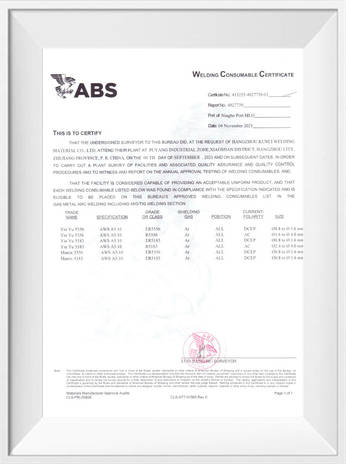
AWS A5.10 ER5154 · ISO 18273 S Al 5154 · ABS Marine Approval
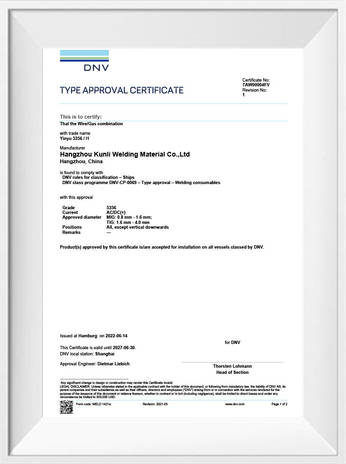
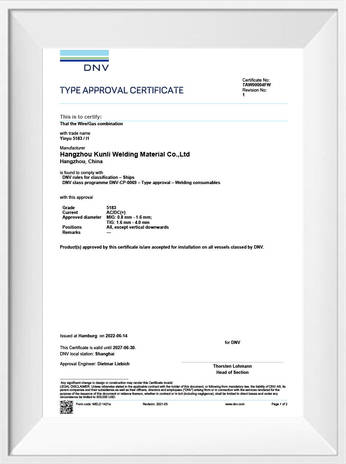
DNV-GL type approved
Shielding Requirements
100% Argon (10-25 L/min) or Ar-He mixture (75/25)
Dew point below -40°C
Field Application Catalog
Marine Construction
Welded aluminum ship hulls, superstructure panels, offshore crew transfer vessels, LNG cargo tank fabrication
Cryogenic Equipment
Liquid natural gas storage tanks, oxygen/nitrogen transport vessels, low-temperature chemical processing lines
Heavy Transport
Aluminum tanker trailers, hopper rail cars, dump truck bodies, container chassis components
Structural Welding
Bridge decks, crane booms, modular building systems, seismic retrofit components
Defense Systems
Armored vehicle hulls, naval ship fittings, missile canister assemblies, tactical bridge modules
Welding Procedure & Troubleshooting
Parameter Selection
For 1.2mm diameter wire: voltage 20-24V, current 120-180A, wire feed speed 4.5-7.5 m/min. Maintain contact tip to work distance of 12-18mm. Use push technique with 10-15 degree travel angle.
Joint Preparation
Remove surface oxide from weld zone using stainless steel brush dedicated to aluminum. Clean with acetone to eliminate hydrocarbon residue. For plate thickness above 8mm, preheat to 100-120°C to reduce cooling rate.
Porosity Control
Check shielding gas hose for leaks. Verify gas flow rate with rotameter. Store wire in humidity controlled environment below 55% RH. Replace contact tip if bore is worn beyond 0.1mm oversize.
Cracking Prevention
Avoid concave bead profiles by maintaining sufficient wire feed. For restrained joints, reduce interpass temperature below 150°C. Use backstep welding sequence for long seam assemblies.
Arc Stability Issues
Inspect drive roll groove condition. Replace Teflon liner after 150kg of wire consumption. Verify electrical connections at work clamp and torch. Use pulse waveform for vertical-up welding positions.
Post-Weld Inspection
Perform dye penetrant testing for surface cracks. Ultrasonic examination for internal defects. Conduct bend tests per AWS B4.0 specifications for procedure qualification.
⛭
Supply Chain & Storage Directives
Receiving Inspection
Verify spool condition and vacuum seal integrity. Check batch certificate for chemical analysis and mechanical test results. Reject any packaging showing moisture ingress or physical damage.
Warehouse Conditions
Store at 10-30°C with humidity range 30-55%. Maintain distance of 1m from exterior walls. Avoid stacking height exceeding 4 pallets. Use first-in-first-out inventory rotation.
Shelf Life Management
Unopened packaging: 36 months from manufacture date. Opened spools: use within 120 hours when stored in workshop environment. For long-term partial spools, use dry cabinet at 35-45°C.
Handling Protocol
Use clean cotton gloves when loading wire into feeder. Prevent contact with oil, grease or coolant mist. Do not set spools on dirty workshop floors. Return protective cover after each shift.
All technical data represents typical values obtained from controlled laboratory testing. Actual performance depends on specific welding parameters, base material condition, joint geometry, and operator skill level. Mechanical properties should be verified through procedure qualification testing.
ER5154 Al-Mg Alloy Wire
Coming From China,
Marketing To The World.
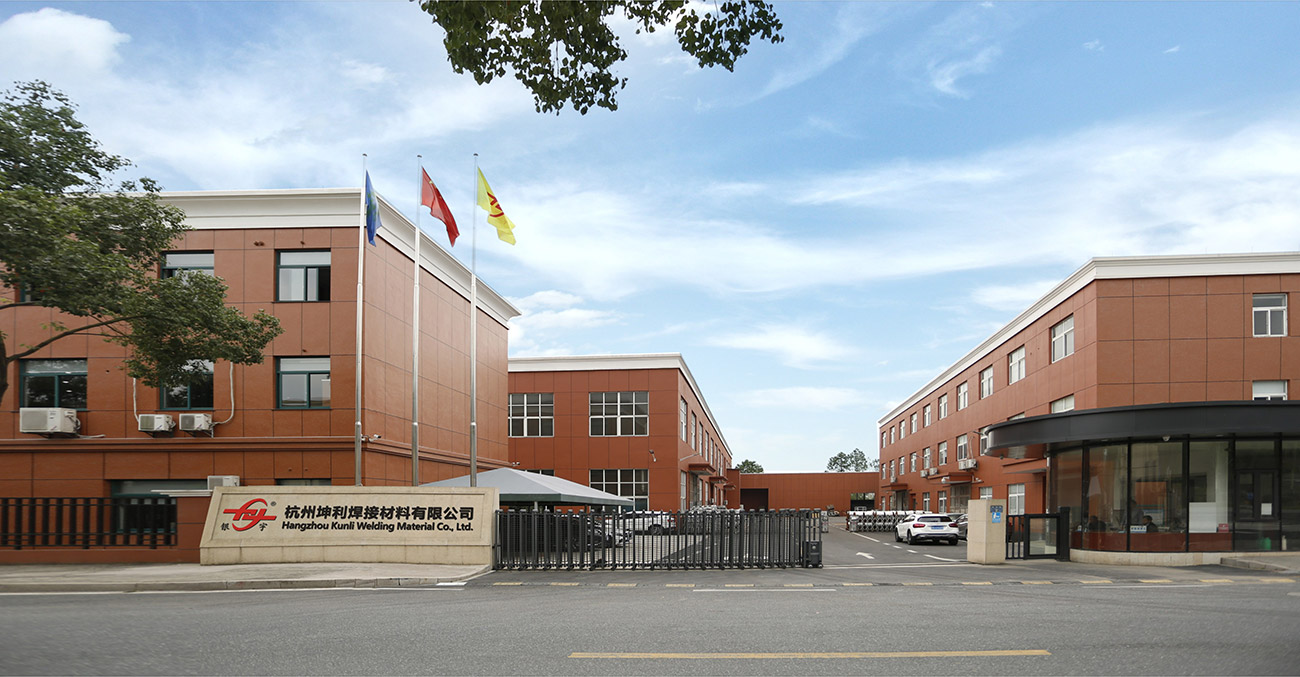
Hangzhou Kunli welding materials Co., Ltd. is located in the industrial zone of Puyang Town, Xiaoshan District, Hangzhou, Zhejiang Province. It is a high-technology and high-performance China Aluminum Welding Wire Manufacturers and
wholesale ER5154 Al-Mg Alloy Wire factory. The company has more than 20 years of aluminum alloy wire production experience, with international advanced aluminum alloy welding wire manufacturing equipment, complete testing equipment, stable production process and strict quality control system. The high-performance
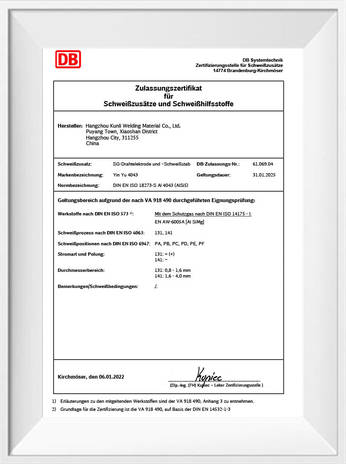
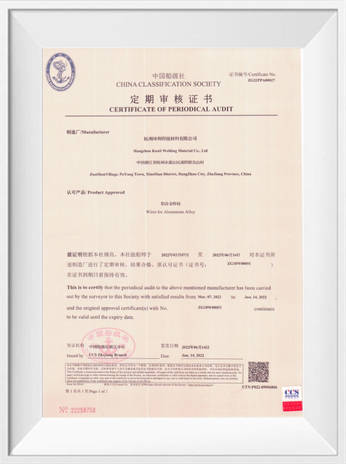
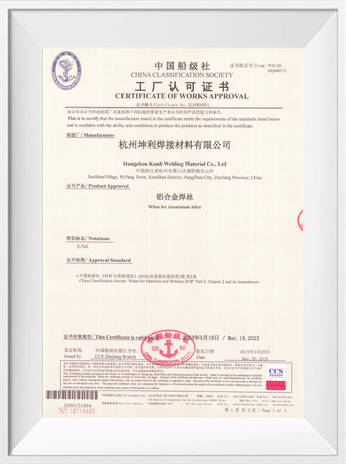
OEM/ODM ER5154 Al-Mg Alloy Wire produced by the company has successfully passed a number of international authoritative certification, such as DB, CE, ABS, DNV, CCS, etc. We have more than 200MT production capacity per month and 50% was exported to over 30 countries such as USA, Mexico, Southeast Asia, Japan, Korea, Australia, New Zealand and etc.
-

30+
USED IN HEAVY INDUSTRY TECHNOLOGY SECTOR
-

35
YEARS OF RESEARCH AND DEVELOPMENT EXPERIENCE
-

200+
COOPERATIVE LARGE-SCALE R & D INSTITUTIONS
-

20+
GLOBAL TRADE COUNTRIES AND REGIONS
Coming From China,
Marketing To The World.
More than 90% of our field operators have professional and technical education background, and have many years of experience in equipment processing and assembly. It is precisely because of this united, dedicated, pioneering, skilled and experienced team that the company's technology and products can be continuously updated and improved.
GET IN TOUCH
Send Us a Message?
Related Products
-
 View More
5154 Aluminum Alloy Welding Wire
-
 View More
ER4043 Silicon Aluminum Welding Wire
-
 View More
ER4047 Aluminum Mig Welding Wire
-
 View More
ER5154 Al-Mg Alloy Wire
-
 View More
ER5087 Magnesium Aluminum Welding Wire
-
 View More
Aluminum Welding Wire ER5183
-
 View More
Aluminum Welding Wire ER5356
-
 View More
ER5554 Aluminum Welding Wire
-
 View More
ER5556 Aluminum Welding Wire
-
 View More
ER1100 Aluminum Welding Wire
-
 View More
ER5754 Aluminum Welding Wire
-
 View More
ER2319 Aluminum Welding Wire
::: Last News :::
-
Why Does Filler Metal Matching Matter in Aluminum Weldi...
Sep 16, 2026
Choosing a filler metal isn't simply a matter of picking an aluminum wire that happens to fit the welding machine sitti...
-
What Causes Feeding Problems With 4943 Aluminum Welding...
Sep 14, 2026
Feeding problems can turn a routine welding job into a genuinely frustrating one fast. The welder may notice uneven wir...
-
Special Al Alloy Welding Wire: Properties & Uses
Sep 09, 2026
Standard aluminum filler wires like ER4043 and ER5356 work fine for everyday fabrication, but they start to fail once w...
-
How Can Spooling Improve Aluminum Welding Wire Handling
Sep 09, 2026
Aluminum welding wire may look simple when viewed as just a continuous strand of metal, but its journey from the spool ...
Industry Information Extension
ER5154 Al-Mg Alloy Wire – Precision Filler for Marine, Cryogenic & Structural Welding
As a Er5154 Almg Alloy Wire.html manufacturer, we match product configuration to the application, operating limits, interfaces and acceptance criteria defined for each project.
Hangzhou Kunli Welding Materials Co., Ltd. is a high-technology manufacturer and supplier of ER5154 Al-Mg alloy wire, engineered for demanding applications where strength, corrosion resistance, and weld integrity are non-negotiable. With over 20 years of aluminum alloy wire production experience, we supply this magnesium-manganese filler metal to shipyards, cryogenic equipment fabricators, heavy transport manufacturers, and structural steel contractors worldwide.
Our ER5154 wire meets AWS A5.10 and ISO 18273 S Al 5154 standards, with certifications including DB, CE, ABS, DNV, and CCS. We produce more than 200 metric tons per month, exporting 50% to over 30 countries. As a Wholesale ER5154 Al-Mg Alloy Wire Factory, we combine advanced manufacturing with strict quality control to deliver consistent batch-to-batch performance.
Product Overview
ER5154 is a magnesium-manganese alloyed filler metal containing 3.1% to 3.9% magnesium with controlled manganese addition of 0.15% to 0.5%. This composition provides higher as-welded strength compared to ER4043 or ER5356 when joining 5xxx series base materials. The manganese content refines grain structure in the weld deposit, improving ductility and fatigue resistance. ER5154 maintains mechanical properties in service temperatures from -196°C to 65°C, supporting cryogenic and marine applications. The alloy system exhibits natural aging stability without heat treatment requirements.
Key Specifications
| Property | Value |
|---|---|
| Magnesium (Mg) | 3.1% – 3.9% |
| Manganese (Mn) | 0.15% – 0.5% |
| Tensile Range | 275 – 320 MPa |
| Elongation | 16 – 20% |
| Hardness | 75 – 85 HB |
| Solidus / Liquidus | 570°C / 640°C |
| Diameter Offering | 0.8mm, 1.0mm, 1.2mm, 1.6mm, 2.0mm (+0 / -0.008mm) |
| Surface Condition | Precision shaved + ultrasonic degreased; residual lubricant below 0.003g/kg |
| Packaging | D300 plastic spool (7kg), K355 drum (50kg), pay-off bin (200kg) |
| Certifications | AWS A5.10 ER5154, ISO 18273 S Al 5154, ABS, DNV-GL |
Application Fit
ER5154 is designed for welding 5xxx series aluminum alloys, particularly in environments where corrosion resistance and low-temperature toughness are critical. Its magnesium content is optimized to prevent sensitization and intergranular corrosion, making it a preferred choice for marine and offshore structures.
- Marine Construction: Welded aluminum ship hulls, superstructure panels, offshore crew transfer vessels, LNG cargo tank fabrication.
- Cryogenic Equipment: Liquid natural gas storage tanks, oxygen/nitrogen transport vessels, low-temperature chemical processing lines.
- Heavy Transport: Aluminum tanker trailers, hopper rail cars, dump truck bodies, container chassis components.
- Structural Welding: Bridge decks, crane booms, modular building systems, seismic retrofit components.
- Defense Systems: Armored vehicle hulls, naval ship fittings, missile canister assemblies, tactical bridge modules.
Technical Performance Framework
- Strength Retention After Welding: Maintains 90-95% of base metal tensile strength in as-welded condition; no post-weld artificial aging required.
- Corrosion Resistance Profile: Passive oxide layer stability in salt spray testing exceeds 2000 hours per ASTM B117; resistance to intergranular attack in chloride environments comparable to 5154 base alloy.
- Thermal Stability: Mechanical property retention at elevated temperatures (150°C for 1000 hours) shows less than 8% reduction in ultimate tensile strength.
- Weld Metal Soundness: Controlled hydrogen content below 0.12ml per 100g aluminum produces radiographic Class I quality welds without centerline porosity or micro-fissuring.
Welding Procedure & Troubleshooting
For 1.2mm diameter wire, typical parameters are voltage 20-24V, current 120-180A, wire feed speed 4.5-7.5 m/min. Maintain contact tip to work distance of 12-18mm. Use push technique with 10-15 degree travel angle.
Joint Preparation: Remove surface oxide from weld zone using stainless steel brush dedicated to aluminum. Clean with acetone to eliminate hydrocarbon residue. For plate thickness above 8mm, preheat to 100-120°C to reduce cooling rate.
Porosity Control: Check shielding gas hose for leaks. Verify gas flow rate with rotameter. Store wire in humidity controlled environment below 55% RH. Replace contact tip if bore is worn beyond 0.1mm oversize.
Cracking Prevention: Avoid concave bead profiles by maintaining sufficient wire feed. For restrained joints, reduce interpass temperature below 150°C. Use backstep welding sequence for long seam assemblies.
Arc Stability Issues: Inspect drive roll groove condition. Replace Teflon liner after 150kg of wire consumption. Verify electrical connections at work clamp and torch. Use pulse waveform for vertical-up welding positions.
Post-Weld Inspection: Perform dye penetrant testing for surface cracks. Ultrasonic examination for internal defects. Conduct bend tests per AWS B4.0 specifications for procedure qualification.
Supply Chain & Storage Directives
Receiving Inspection: Verify spool condition and vacuum seal integrity. Check batch certificate for chemical analysis and mechanical test results. Reject any packaging showing moisture ingress or physical damage.
Warehouse Conditions: Store at 10-30°C with humidity range 30-55%. Maintain distance of 1m from exterior walls. Avoid stacking height exceeding 4 pallets. Use first-in-first-out inventory rotation.
Shelf Life Management: Unopened packaging: 36 months from manufacture date. Opened spools: use within 120 hours when stored in workshop environment. For long-term partial spools, use dry cabinet at 35-45°C.
Handling Protocol: Use clean cotton gloves when loading wire into feeder. Prevent contact with oil, grease or coolant mist. Do not set spools on dirty workshop floors. Return protective cover after each shift.
Quality Assurance & Compliance
Our manufacturing facility is equipped with internationally advanced production lines and a complete testing laboratory, including SHIMADZU PDA 5500-Optical emission spectrograph, LEICA DM2550 Metallographic Microscope, and OTC A-V6 Welding robot system. Each batch undergoes chemical composition analysis, mechanical testing, and welding performance verification to ensure compliance with AWS A5.10 and ISO 18273.
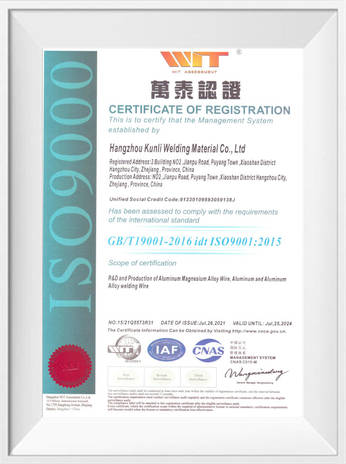
We hold certifications including DB, CE, ABS, DNV, and CCS, and our quality management system is ISO9001, ISO14000, and ISO18001 certified. Our close cooperation with Beijing Nonferrous Metals Research Institute and Central South University supports continuous alloy development and process optimization.
Information We Use to Configure Your Solution
To prepare a precise quotation and product configuration, we need the following project details:
- Base material grade and thickness
- Welding process (MIG, TIG, or automated)
- Required diameter and packaging preference
- Application environment (marine, cryogenic, structural, etc.)
- Production volume and delivery schedule
- Any specific certification or documentation requirements
Our engineering team will recommend the optimal wire grade and packaging to match your welding parameters and quality standards.
Related Products
Explore our full range of aluminum welding wires to find the right match for your application:
- Aluminum Welding Wire ER5356 – Higher magnesium for increased strength
- Aluminum Welding Wire ER5183 – For 5xxx series with improved toughness
- Aluminum Welding Wire ER5087 – High-strength filler for marine structures
- ER4043 Silicon Aluminum Welding Wire – For 6xxx series and casting repair
FAQs
What is the difference between ER5154 and ER5356?
ER5154 has lower magnesium (3.1-3.9%) compared to ER5356 (4.5-5.5%), offering superior resistance to intergranular corrosion and better stability at temperatures above 65°C. ER5356 provides higher tensile strength but is more susceptible to sensitization in marine environments.
Can ER5154 be used for cryogenic applications?
Yes, ER5154 maintains mechanical properties down to -196°C, making it suitable for LNG tanks and other cryogenic equipment. Its low-temperature toughness and corrosion resistance are key advantages.
What packaging options are available?
We offer D300 plastic spools (7kg), K355 drums (50kg), and pay-off bins (200kg). Custom packaging can be arranged based on your production needs.
How do you ensure consistent quality?
Each batch is tested in our in-house laboratory for chemical composition, mechanical properties, and welding performance. We also maintain strict process control and traceability from raw material to finished product.
What is the typical lead time?
Lead time depends on order quantity and specifications. For standard sizes and packaging, we typically ship within 2-3 weeks after order confirmation. Please contact us for specific lead times.
QUICK LINKS
PRODUCT
CONTACT US
-
Jianpu Road no.2 Puyang Town Xiaoshan District Hangzhou Zhejiang China 311255
-
+86-0571-82403878
-
+86-0571-82403208
-
rich@chinayinyu.com
MOBILE TERMINAL
BE THE FIRST TO KNOW
Copyright © Hangzhou Kunli Welding Materials Co., Ltd. Rights Reserved.
