English
 Deutsch

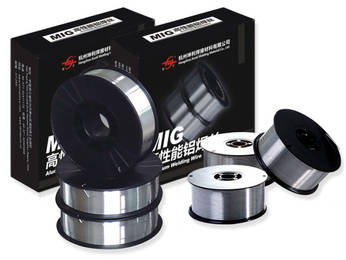
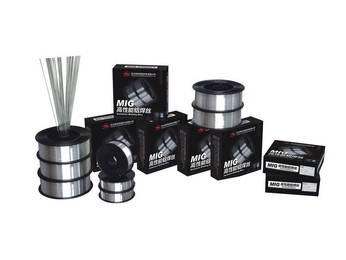
Aluminum Alloy Wire for 3D Printing: Properties, Applications, and Advantages in Metal Additive Manufacturing
Article Directory
- 1 Alloy Performance Comparison: Key Properties Across Common Types
- 2 Industrial Applications & Performance Profiles
- 3 Aluminum Alloy Wire vs. Powder-Based 3D Printing
- 4 Manufacturing Process: From Alloy to Production Wire
- 5 How to Select the Right Aluminum Wire for Your Application
- 6 Frequently Asked Questions About Aluminum Alloy Wire 3D Printing
Aluminum alloy wire for 3D printing transforms metal additive manufacturing from a prototype technology into a production-scale solution. Wire-fed systems deliver 50-100x faster deposition than powder-based methods while cutting material costs by 40-60%. This technical guide covers selection criteria, industrial applications, and manufacturing advantages.
Alloy Performance Comparison: Key Properties Across Common Types
Industrial Applications & Performance Profiles
Aerospace Manufacturing
Lightweight structural components and aircraft prototypes leverage aluminum's 2.7 g/cm³ density and high strength-to-weight ratio.
Automotive Production
Vehicle frames, suspension brackets, and engine blocks printed with rapid prototyping timelines and optimized weight distribution.
Marine & Offshore
Ship components and seawater-resistant structures benefit from aluminum's natural corrosion resistance and salt-spray durability.
Industrial Equipment
Large-format tooling, machinery frames, and customized components produced on-demand with minimal lead time and waste.
Aluminum Alloy Wire vs. Powder-Based 3D Printing
| Performance Metric | Aluminum Wire | Aluminum Powder |
| Material Utilization | 85-95% | 60-75% |
| Deposition Speed | 8-20 kg/hour | 0.1-0.5 kg/hour |
| Equipment Cost | $200K-500K | $400K-1M+ |
| Material Cost per kg | $50-80 | $150-300 |
| Component Size | Unlimited (scalable) | Limited by build chamber |
| Storage Safety | Low hazard | High flammability risk |
Manufacturing Process: From Alloy to Production Wire
Alloy Composition Control
Raw aluminum, magnesium, silicon, copper, and trace elements are precisely measured and melted in controlled furnaces. Composition accuracy ensures consistent 3D printing behavior and mechanical properties across batches.
Casting & Extrusion
Molten alloy is cast into ingots, then extruded through dies to create rough wire. This forms the continuous feedstock required for additive manufacturing systems.
Wire Drawing
Extruded material passes through progressive drawing dies to achieve precise diameter tolerance (typically ±0.1mm). This ensures reliable feeding in WAAM and laser wire systems.
Surface Treatment
Wire surfaces are cleaned to remove oxides and contaminants. Lubrication coatings are applied to reduce friction during feeding and improve printing stability.
Quality Inspection
Dimensional accuracy, chemical composition, surface quality, and mechanical properties are tested. Only wire meeting strict specifications is spooled and shipped to manufacturing facilities.
How to Select the Right Aluminum Wire for Your Application
Matching Alloy to Process
WAAM systems require high fluidity and stable arc behavior (AlSi10Mg, AlSi7). Laser wire processes demand precise melting control (ER5356, ER5754). Cold-wire processes need excellent ductility. Verify your equipment specifications before selecting alloy composition.
Mechanical Property Requirements
Aerospace applications demand high strength (ER2319: 280+ MPa). Marine environments require corrosion resistance (ER5356: superior seawater performance). Industrial tooling prioritizes dimensional stability (AlSi7: low thermal distortion). Match wire selection to end-use performance demands.
Environmental Conditions
Saltwater exposure demands Al-Mg alloys (ER5356, ER5754). High-temperature service requires heat-treatable alloys (AlSi10Mg). Outdoor UV exposure needs UV-resistant coatings. Specify wire composition that survives your component's operational environment.
Cost-Benefit Analysis
High-end aerospace wire ($60-80/kg) ensures reliability. General industrial applications favor mid-range options ($45-60/kg). Compare material cost against scrap rates, rework expenses, and equipment compatibility to determine true TCO across production volumes.
Frequently Asked Questions About Aluminum Alloy Wire 3D Printing
What is the typical deposition rate for aluminum wire 3D printing?
Wire-fed systems deposit 8-20 kg per hour depending on wire diameter, process type, and power settings. This is 50-100x faster than powder-based systems (0.1-0.5 kg/hour). For large components, this translates to production cycles measured in hours rather than days.
Can any aluminum welding wire be used for 3D printing?
Not all welding wires work for additive manufacturing. 3D printing requires specific alloy compositions, tighter diameter tolerances (±0.1mm), and cleaner surfaces. WAAM systems specifically demand ER5356, ER5754, ER2319, and aluminum-silicon alloys designed for controlled deposition. Always verify wire specifications with your equipment manufacturer.
What is the cost advantage of aluminum wire versus aluminum powder?
Material cost averages $50-80/kg for wire versus $150-300/kg for powder—a 3-6x cost difference. Equipment costs also favor wire ($200-500K versus $400K-1M+ for powder). Combined with 85% utilization versus 60% for powder, wire-based systems reduce total manufacturing cost by 40-60% for large components.
How does aluminum wire handle corrosion in marine environments?
Aluminum naturally forms a protective oxide layer. Al-Mg alloys (ER5356, ER5754) provide superior seawater resistance due to higher magnesium content. ER5356 rated for submerged marine service without special coatings. For maximum durability, anodizing post-printed components adds additional protection.